Made-to-order manufacturing is reshaping the sheet-metal industry. Fabricators are increasingly handling customer-specific designs, variable batch sizes, frequent engineering revisions, and tighter production schedules. These conditions are encouraging workshops to invest in machines that can perform clearly defined tasks while remaining practical for everyday production.
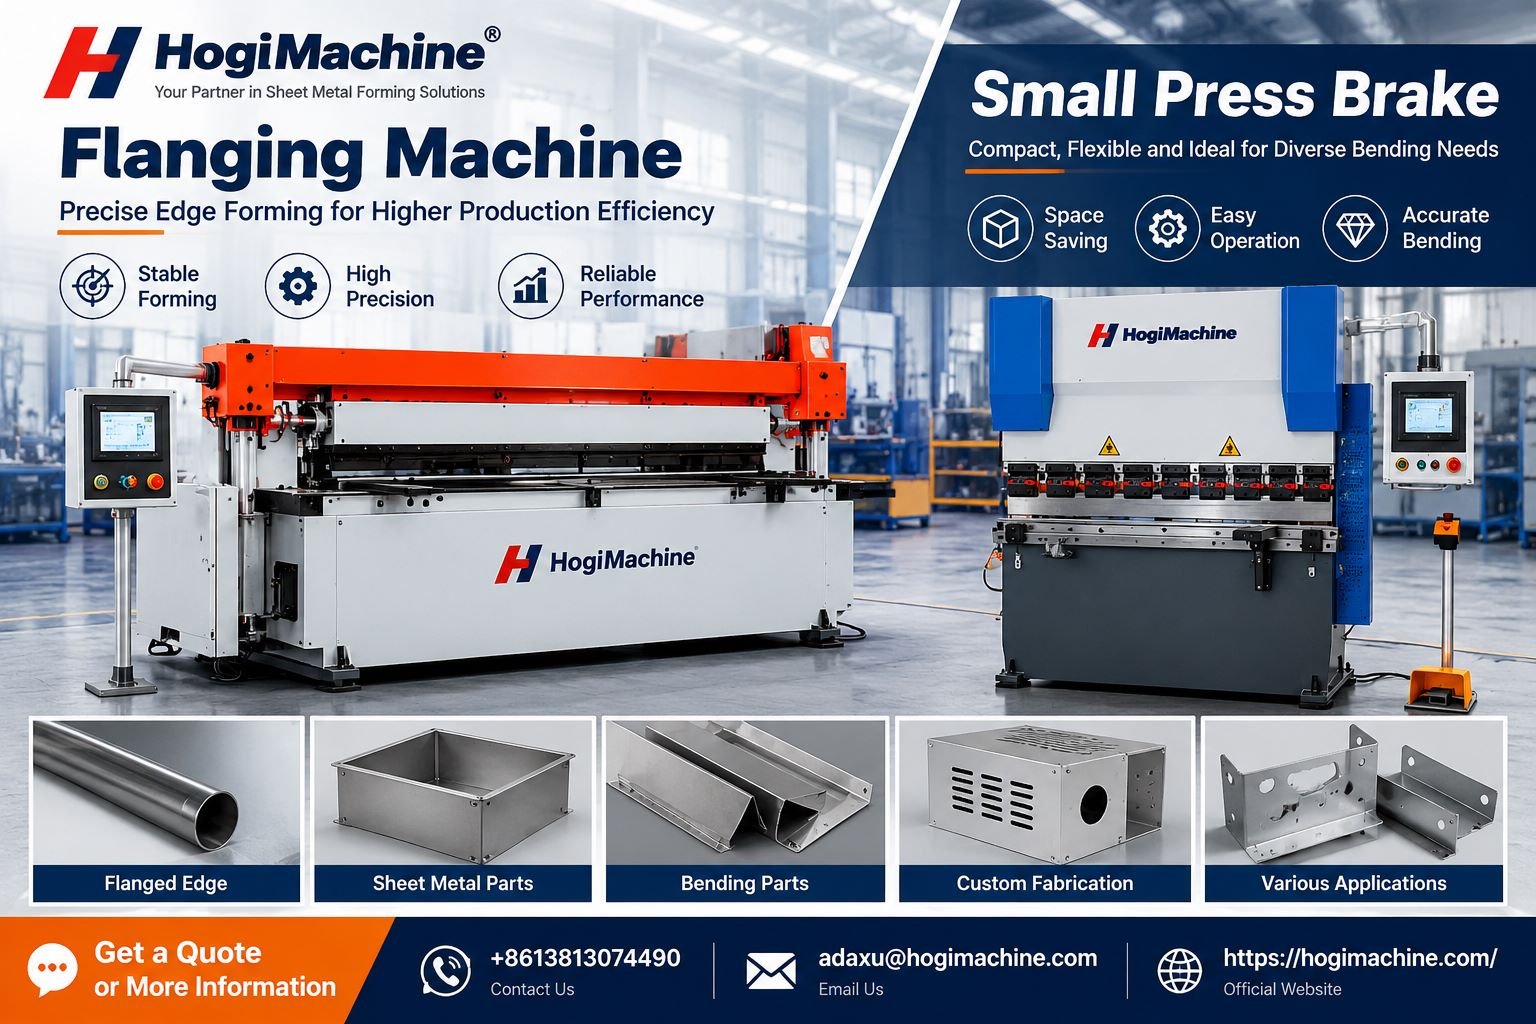
The Flanging machine is becoming increasingly relevant for manufacturers that need controlled edge forming, while the small press brake provides a practical route for bending suitable compact components. Instead of evaluating these machines only by speed, modern buyers are looking at accuracy, setup efficiency, tooling, workflow integration, operator usability, and long-term production value.
Made-to-Order Manufacturing Creates New Forming Challenges
Standardized mass production allows manufacturers to optimize one process around large quantities. Custom fabrication operates differently.
A workshop may receive drawings for different materials, component sizes, bend configurations, and order quantities throughout the week.
Equipment therefore needs to fit a changing production environment.
A Flanging machine can provide a dedicated process for products requiring repeatable formed edges. Meanwhile, other bending operations can be assigned to press brake equipment according to component size and required capacity.
This division of work can make production planning more predictable.
Flanging Can Prepare Components for the Next Manufacturing Stage
Flanging should not be considered only as an isolated forming operation.
The quality and position of a flange can affect what happens afterward.
A formed edge may become part of a welded assembly, provide a joining surface, strengthen a panel, or interact with another component.
This means a Flanging machine contributes to downstream productivity when the resulting geometry is consistent with assembly requirements.
Manufacturers should therefore evaluate flange quality according to the function it performs in the finished product rather than appearance alone.
Small Press Brake Equipment Creates Dedicated Bending Capacity
Production bottlenecks often occur when many different jobs compete for the same machine.
A large press brake may be processing substantial panels while operators are waiting to produce a small group of brackets.
Creating dedicated capacity for compact work can reduce this conflict.
A small press brake can handle suitable jobs while larger machinery continues with work requiring greater dimensions or forming capacity.
For workshops with a varied order book, this approach can help separate different classes of bending work and make scheduling easier.
Rapid Engineering Changes Require Responsive Equipment
Custom fabrication projects frequently evolve after the first prototype.
A customer may request a different hole position, revised bend, altered flange, or modified assembly feature.
When quantities are still small, manufacturers need to respond without creating excessive disruption.
Compact forming equipment can be valuable during this phase.
If the revised component falls within the capability of a small press brake, the workshop can produce another sample or short batch without reorganizing a major production schedule.
Once the design is approved, controlled job information can be retained for repeat manufacturing.
Design for Manufacturing Can Simplify Forming
Product design has a direct influence on fabrication difficulty.
Features that appear simple in CAD can sometimes create unnecessary tooling, handling, or forming challenges.
Early communication between designers and manufacturing teams can help identify these concerns.
For example, engineers can review whether flange geometry is practical, whether bends provide suitable tooling access, and whether previously formed sections interfere with later operations.
Design-for-manufacturing review can therefore reduce avoidable complexity before the component reaches the Flanging machine or press brake.
Tool Changes Should Be Managed Systematically
High-mix production may require frequent tooling changes.
If tooling is poorly organized, operators can lose valuable time searching for the correct setup.
A structured tooling area can improve this process.
Tools can be identified, stored, inspected, and returned to defined locations after use. Frequently required tools can be positioned for convenient access where appropriate.
For a small press brake handling multiple jobs per shift, efficient tooling management can contribute significantly to overall productivity.
The same discipline can support dedicated flanging work.
First-Off Parts Can Protect the Remaining Batch
When a new setup is completed, producing an entire batch immediately creates unnecessary risk.
A first-off component can be manufactured and checked before full production continues.
The verification should focus on characteristics relevant to the component’s function and drawing requirements.
If a problem is discovered, operators can correct the setup before additional material is processed.
For custom and lower-volume jobs, this approach is particularly valuable because losing even a few workpieces may represent a meaningful percentage of the total order.
Production Traceability Supports Repeat Customers
Repeat customers expect the same component to be produced correctly when they reorder it.
This can become difficult if manufacturing information is scattered across handwritten notes or dependent on operator memory.
Controlled production records can help preserve information such as drawing revision, material, tooling, operation sequence, and inspection requirements.
For recurring Flanging machine work, records can provide useful references when a component returns after a long interval.
Digital documentation can also make engineering changes easier to track.
Compact Equipment Can Support Better Space Utilization
Manufacturing floor space needs to accommodate more than machines.
Factories also require material storage, work-in-progress areas, tooling, inspection stations, assembly space, maintenance access, and safe movement routes.
A small press brake can be attractive where production requirements do not justify substantially larger equipment.
However, machine footprint should be evaluated together with the operating area required around it.
Enough space should remain available for safe workpiece handling, tooling changes, servicing, and normal operation.
Equipment Value Should Be Measured Over Time
Purchase price is an obvious consideration, but it does not describe the complete value of fabrication machinery.
Businesses should also consider machine utilization, maintenance, tooling, training, available production work, and the ability to reduce bottlenecks.
A dedicated Flanging machine may create value if recurring flange work currently consumes excessive time on other equipment.
Similarly, compact bending capacity can be commercially useful when a workshop has sufficient suitable work to keep it productive.
Investment should therefore be connected to actual manufacturing demand.
Frequently Asked Questions
What is a Flanging machine?
A Flanging machine is metal-forming equipment used to create a flange or formed edge on a workpiece for assembly, reinforcement, joining, or other manufacturing requirements.
What is a small press brake?
A small press brake is compact equipment designed to perform bending operations on sheet-metal components within its specified working and forming capacity.
Why use dedicated flanging equipment?
Dedicated equipment can make recurring flange operations easier to standardize and separate them from unrelated forming work.
Is a compact press brake suitable for job shops?
It can be particularly useful in job-shop environments where suitable small components, prototypes, and short production batches are common.
What determines press brake capacity requirements?
Material properties, sheet thickness, bend length, tooling, component geometry, and the required forming operation all influence capacity requirements.
What is first-off inspection?
First-off inspection verifies an initial component after setup before the remaining production batch is manufactured.
Why is tooling organization important?
Organized tooling can reduce preparation time, simplify setups, and help ensure operators select the appropriate tools.
Can forming equipment help with prototype development?
Yes. Suitable forming equipment can support prototype and pre-production components when the required operations remain within machine capabilities.
Why should production records be retained?
Records can help manufacturers reproduce previous jobs and identify the correct setup when customers place repeat orders.
What should be evaluated before buying a flanging or bending machine?
Buyers should consider materials, component dimensions, forming requirements, production quantities, machine capacity, tooling, available space, maintenance, training, and expected utilization.
Media Contact
Sheet Metal Forming Machinery Enquiries
Contact: +86 138 1307 4490
Email: adaxu@hogimachine.com
Official Website: hogimachine.com