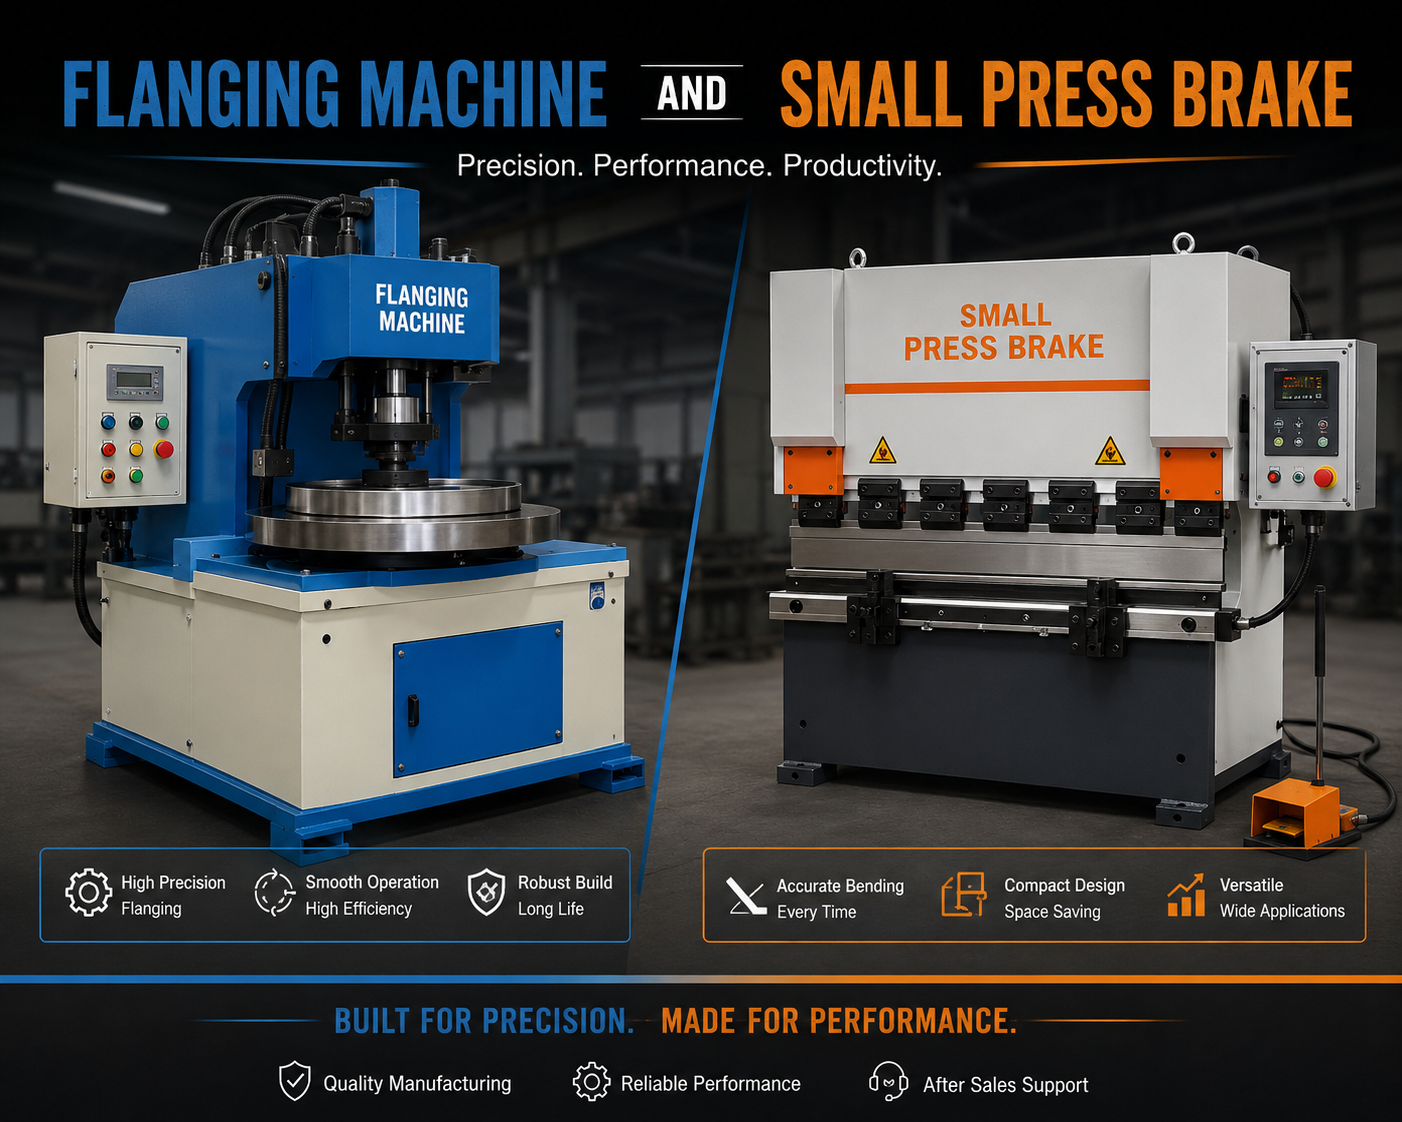
Efficient sheet metal manufacturing depends on choosing machines that match the exact forming requirement. Among the most practical machines used in fabrication units are the flanging machine and small press brake. These machines perform different operations, yet both contribute to better accuracy, faster production, and improved component quality.
A flanging machine is designed mainly for shaping the edges of sheet metal parts, while a small press brake is used for bending metal into precise angles and profiles. For workshops handling customized components, short production runs, HVAC parts, enclosures, tanks, brackets, and industrial fabrication, these machines can significantly improve workflow.
How Modern Sheet Metal Forming Has Improved
Traditional metal forming often relied heavily on manual bending, hammering, and repeated adjustments. These methods required more labor and could produce inconsistent results.
Modern forming machines provide controlled movement and repeatable pressure. This helps manufacturers maintain similar dimensions across multiple parts while reducing unnecessary rework.
Major improvements include:
- Better dimensional accuracy
- Faster forming cycles
- Reduced operator fatigue
- Improved part consistency
- Lower rejection rates
- Easier production planning
- Better surface finish
Using appropriate equipment also makes it easier to manufacture complex parts without excessive manual correction.
What Makes a Flanging Machine Different?
A flanging machine reshapes the outer or inner edge of a sheet metal component to create a flange. This flange may be used for joining two components, improving stiffness, preparing a welding surface, or strengthening the edge.
Flanging is especially important when manufacturing circular, cylindrical, or curved metal components.
Typical Flanging Process
The operator positions the component correctly within the machine. Forming rollers or dies then apply controlled pressure to the edge.
Instead of forcing the material into shape instantly, many machines gradually form the flange. This controlled process helps prevent cracking, wrinkling, and excessive material distortion.
Common Flange Shapes
Depending on tooling and machine design, manufacturers can create:
- Straight flanges
- Curved flanges
- Internal flanges
- External flanges
- Circular rims
- Raised edges
This flexibility makes flanging equipment useful across many manufacturing industries.
Industries That Depend on Flanging Equipment
The flanging machine is widely used where sheet metal edges require consistent forming.
Typical industries include:
- Tank manufacturing
- HVAC production
- Automotive fabrication
- Pressure vessel manufacturing
- Industrial ducting
- Metal drum production
- Food-processing equipment
- Ventilation systems
- Exhaust component manufacturing
- General engineering workshops
The machine becomes particularly valuable when many identical components must be produced with similar flange dimensions.
Why Small Press Brakes Are Valuable
A small press brake provides professional bending capability without requiring the space associated with large industrial press brakes.
The machine works by placing sheet metal over a die and forcing a punch downward. This movement creates a controlled bend at a predetermined location.
Small machines are often selected by workshops that produce brackets, boxes, panels, covers, and custom sheet metal components.
Benefits of Using a Small Press Brake
The small press brake offers a combination of flexibility and compact design.
Advantages include:
- Easy installation in smaller workshops
- Accurate bend angles
- Flexible tooling options
- Quick setup for short runs
- Suitable prototype manufacturing
- Reduced floor-space requirements
- Good repeatability
- Ability to produce multiple profiles
Modern versions may include programmable backgauges and digital angle controls to further improve production accuracy.
Understanding the Role of Press Brake Tooling
A press brake cannot produce consistent parts without suitable tooling.
Punch Selection
The punch determines the upper forming profile and strongly influences the final bend.
Die Opening
The lower die opening must be selected according to material thickness and desired bend radius.
Tool Condition
Damaged or worn tools may create inaccurate bends, scratches, inconsistent angles, and poor finished surfaces.
Regular tooling inspection is therefore an important part of press brake maintenance.
Flanging Machine and Small Press Brake: Practical Comparison
| Factor | Flanging Machine | Small Press Brake |
| Primary purpose | Edge forming | Sheet bending |
| Best for | Rims, flanges, round parts | Angles, brackets, panels |
| Main tooling | Rollers/forming dies | Punch and die |
| Circular work | Very suitable | Limited |
| Straight bending | Limited | Excellent |
| Custom job flexibility | Moderate | High |
| Repetitive production | Excellent | Excellent |
| Typical workshop use | Specialized forming | General fabrication |
In many factories, these machines are used together instead of replacing one another.
Choosing a Flanging Machine for Your Workshop
Before buying a flanging machine, manufacturers should understand their normal production requirements.
Important parameters include:
Material Thickness
The machine must provide sufficient forming power for the maximum material thickness used.
Material Type
Mild steel, stainless steel, aluminum, copper, and other metals respond differently during forming.
Workpiece Dimensions
Check whether the machine can handle the required minimum and maximum component diameters.
Flange Requirements
The desired flange width, radius, direction, and angle should be compatible with the available tooling.
Production volume should also be considered. Higher-volume applications may benefit from automated or CNC-controlled systems.
Selecting the Right Small Press Brake
A small press brake should be selected according to actual bending needs rather than simply choosing the highest tonnage available.
Important factors include:
- Maximum bending length
- Material thickness
- Material tensile strength
- Required bending force
- Tooling compatibility
- Backgauge accuracy
- Control system
- Frame rigidity
- Safety features
- Service availability
Manufacturers should also consider future production requirements so that the machine does not become undersized too quickly.
Production Problems and How to Reduce Them
Even high-quality equipment can produce poor results if setup conditions are incorrect.
Uneven Bending
This may result from poor tooling alignment, inconsistent material thickness, or machine deflection.
Cracking During Flanging
Cracking can occur when the flange radius is too small or material is formed too aggressively.
Dimensional Variation
Incorrect backgauge positioning or inconsistent workpiece placement can cause size differences between parts.
These issues can often be reduced through proper machine setup and operator training.
Tips for Increasing Machine Productivity
Manufacturers can improve daily output by following simple production practices:
- Record successful machine settings
- Organize commonly used tooling
- Inspect machines before each shift
- Check first-off components
- Maintain proper lubrication
- Keep forming surfaces clean
- Replace damaged tools promptly
- Train operators in safe setup procedures
- Use standardized inspection methods
Good organization can often improve productivity without increasing machine speed.
Frequently Asked Questions
1. What is a flanging machine mainly used for?
A flanging machine forms sheet metal edges into flanges, rims, or reinforced profiles.
2. Why are flanges added to metal components?
Flanges can increase strength, improve joining, support welding, and simplify assembly.
3. Can a flanging machine process stainless steel?
Yes, when the machine capacity and tooling are suitable for the selected stainless steel grade.
4. What is a small press brake used for?
A small press brake bends sheet metal into accurate angles, brackets, channels, boxes, and similar parts.
5. Is a small press brake suitable for custom fabrication?
Yes. Its flexible tooling makes it particularly useful for customized and short-run components.
6. What determines required press brake tonnage?
Material thickness, tensile strength, bending length, die opening, and bending method affect required tonnage.
7. Can press brakes create 90-degree bends?
Yes. Appropriate tooling and machine settings can produce accurate 90-degree and other bend angles.
8. Why does metal crack while flanging?
Possible causes include an excessively tight radius, poor material quality, wrong tooling, or excessive forming pressure.
9. What is press brake springback?
Springback is the partial return of metal toward its original shape after bending pressure is released.
10. How can press brake accuracy be improved?
Correct tooling, accurate backgauge positioning, machine alignment, test bending, and springback compensation improve accuracy.
11. Do flanging machines require special tooling?
Yes. Tooling should match the required flange dimensions, workpiece shape, and material properties.
12. How often should forming machines be inspected?
Routine checks should be performed regularly, while detailed maintenance should follow the manufacturer’s recommended schedule.