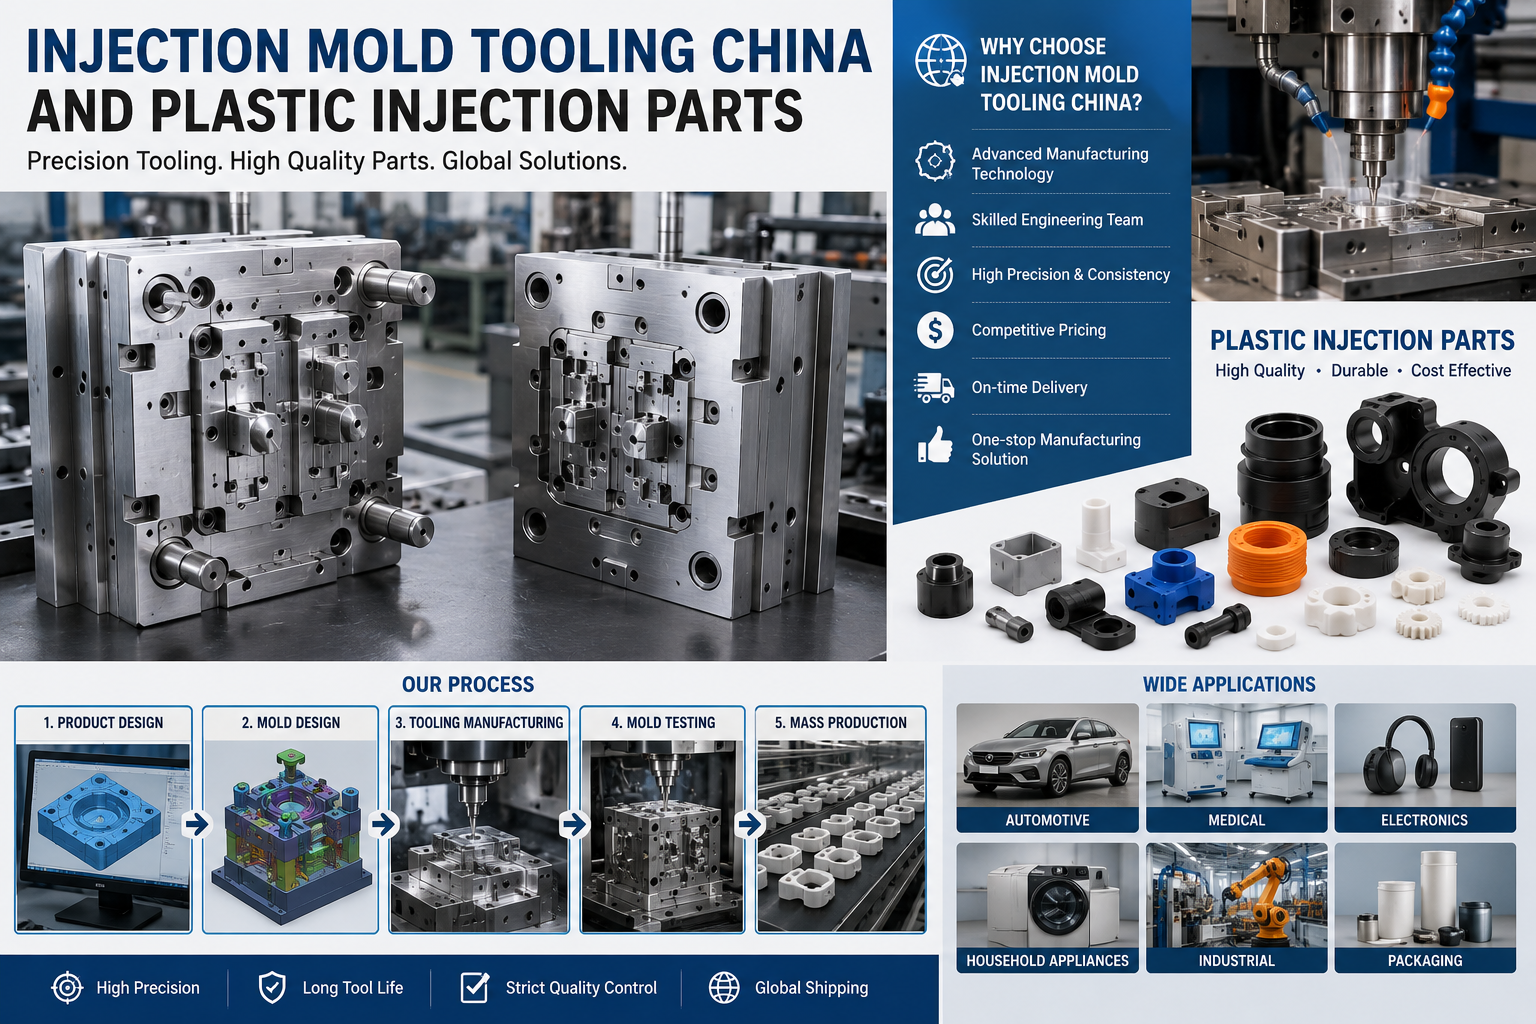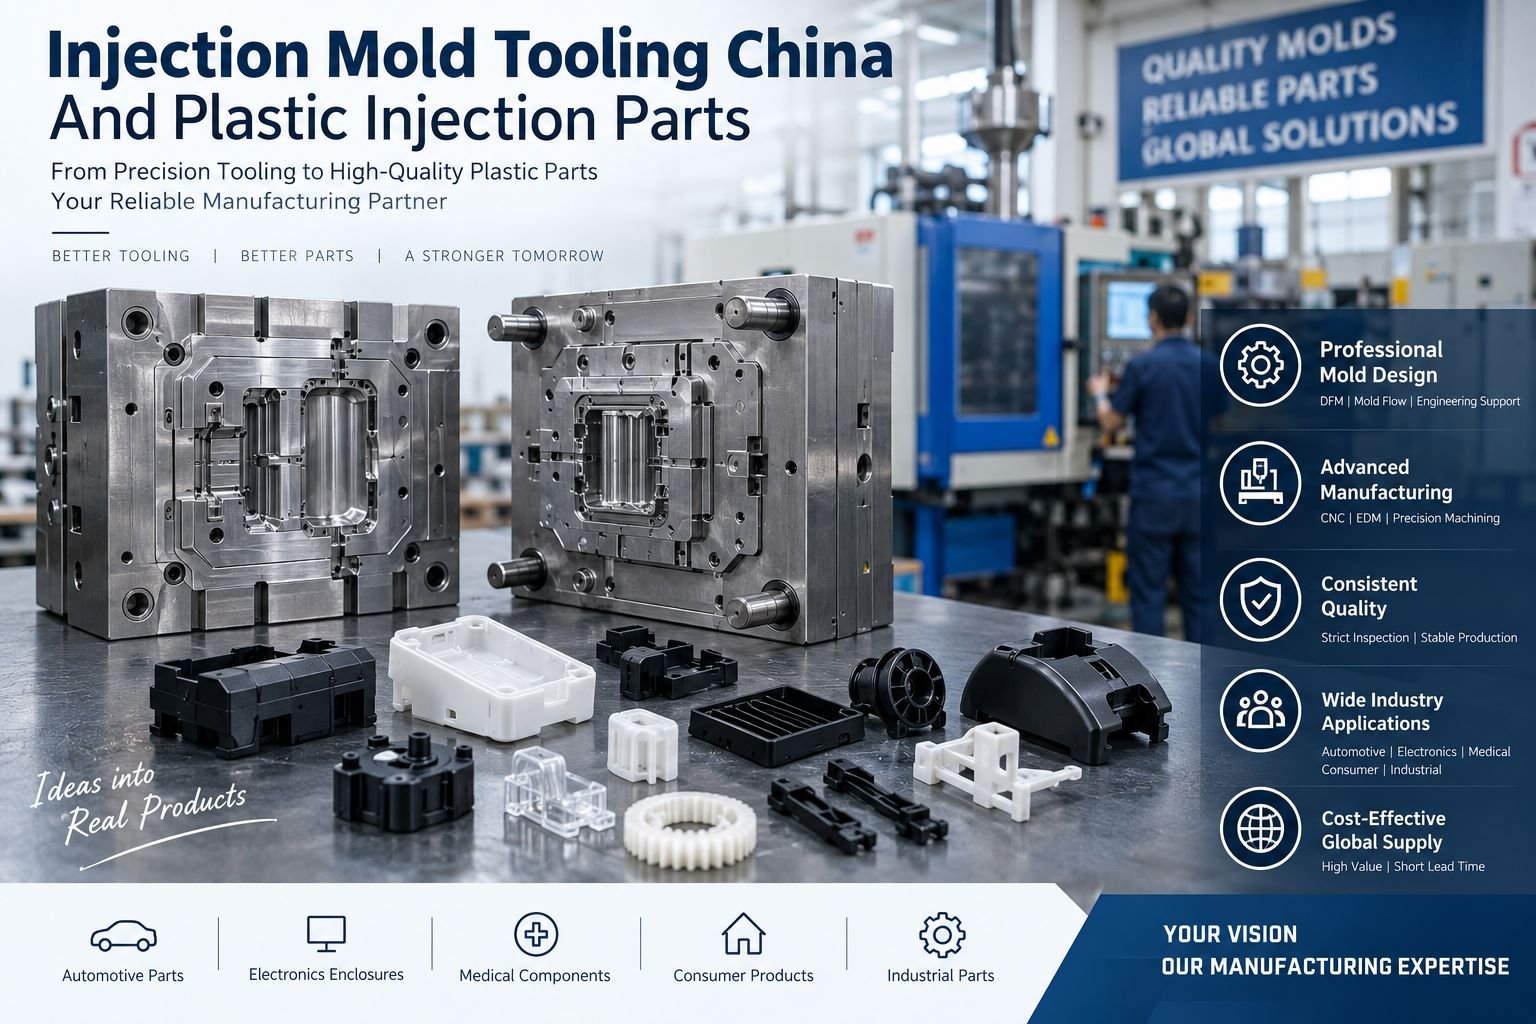
For companies planning custom plastic products, selecting reliable Injection Mold Tooling China services can play an important role in achieving consistent quality and efficient mass production. A well-made mold helps manufacturers produce accurate Plastic Injection Parts repeatedly while controlling manufacturing time, material waste, and overall production cost.
In this blog, we explore how injection mold tooling works, why mold quality matters, which factors influence molded components, and what businesses should consider before starting a plastic injection molding project.
Why Injection Mold Tooling Is So Important
An injection mold is more than a metal tool with a cavity. It is a precision manufacturing system designed to create the same component thousands or even millions of times.
The mold determines important product characteristics such as:
- Component dimensions
- Surface appearance
- Wall thickness
- Parting lines
- Gate marks
- Dimensional consistency
- Cooling performance
- Ejection quality
Even an advanced injection molding machine cannot consistently produce good parts if the mold itself has engineering problems.
This is why professional Injection Mold Tooling China manufacturers normally focus heavily on mold design before machining begins.
Starting With a Manufacturable Product Design
A successful injection molding project starts with the product design.
A designer may create a component that looks excellent on screen but contains features that are difficult or expensive to manufacture.
Before mold production, engineers usually review the model for manufacturability.
Important areas include:
- Uniform wall thickness
- Suitable draft angles
- Rib dimensions
- Boss design
- Undercuts
- Sharp corners
- Parting-line locations
- Gate positioning
- Ejection requirements
Making changes during this stage is generally easier than correcting a finished mold.
Good design planning also helps reduce potential problems in Plastic Injection Parts, including sink marks, warpage, short shots, and difficult ejection.
How Injection Mold Tooling China Is Manufactured
The tooling process involves several engineering and machining stages.
After reviewing the component design, engineers prepare the mold structure according to product size, material, production quantity, and machine specifications.
A typical workflow may include:
- Product and tooling analysis
- Mold structure development
- Mold steel selection
- Core and cavity machining
- EDM processing
- Cooling-channel machining
- Slide and lifter manufacturing
- Mold fitting and assembly
- Surface polishing or texturing
- Initial mold testing
After assembly, the mold is installed in an injection molding machine for testing.
The first samples allow engineers to examine dimensions, filling behavior, surface appearance, shrinkage, and ejection.
Any required tooling adjustments can then be completed before mass production.
Turning Plastic Resin Into Finished Components
Once the mold is ready, production of Plastic Injection Parts can begin.
Plastic resin is supplied in pellet form and fed into the molding machine. Depending on the material, the resin may first require drying to remove moisture.
Inside the machine, a heated barrel melts the plastic.
The molten material is then injected into the closed mold under pressure.
After filling the cavity:
- Holding pressure compensates for material shrinkage.
- Cooling channels remove heat.
- The plastic becomes solid.
- The mold opens.
- Ejector pins release the component.
The entire cycle can then repeat automatically.
Production efficiency depends on mold design, plastic material, component thickness, cooling performance, and machine settings.
Choosing Plastic Materials Carefully
There are many materials available for manufacturing Plastic Injection Parts, and each one behaves differently during processing and use.
Common choices include:
| Material | Key Benefit | Typical Application |
| ABS | Good toughness and appearance | Electronic housings |
| PP | Lightweight and chemical resistant | Packaging and containers |
| PC | Excellent impact resistance | Protective covers |
| PA/Nylon | Strong and wear resistant | Mechanical components |
| POM | Low friction and dimensional stability | Precision gears |
| TPE | Flexible and soft | Handles and seals |
Material should be chosen based on actual product requirements.
For example, an automotive component exposed to engine heat needs different properties from a cosmetic packaging component.
Manufacturers should consider temperature, strength, flexibility, chemical exposure, UV resistance, appearance, compliance requirements, and expected lifespan.
Understanding Mold Cavities and Production Volume
Production requirements influence mold construction.
A single-cavity mold produces one product during every injection cycle.
This setup can be practical for:
- Lower production quantities
- Large components
- Prototype development
- Complex products
A multi-cavity mold produces several components simultaneously.
For high-volume Plastic Injection Parts, multi-cavity tooling may significantly increase production output.
However, every cavity must receive plastic evenly. Poor runner balancing can cause differences between parts.
Experienced Injection Mold Tooling China suppliers therefore carefully design the runner, gating, and cooling systems when developing multi-cavity molds.
Why Cooling Can Affect Part Quality
Cooling is one of the most important stages of injection molding.
Once plastic enters the cavity, heat must be removed in a controlled manner before the component can be ejected.
If cooling is uneven, the product may shrink differently across various areas.
Possible problems include:
- Warped components
- Longer cycle times
- Dimensional variation
- Surface defects
- Internal stress
Effective cooling-channel design can improve both quality and productivity.
Reducing unnecessary cooling time by even a few seconds can create meaningful production improvements when manufacturing hundreds of thousands of parts.
Common Problems in Plastic Injection Parts
Injection molding is highly repeatable, but problems can occur when tooling, materials, or processing parameters are incorrect.
Common defects include:
Sink Marks: Depressions appearing on thicker areas of a component.
Flash: Excess plastic forming around mold separation areas.
Short Shots: Incomplete parts caused by insufficient cavity filling.
Warpage: Product distortion after cooling.
Weld Lines: Visible lines formed where separate plastic flow fronts meet.
Burn Marks: Darkened areas caused by trapped air or excessive heat.
Identifying the root cause is important because the solution may involve tooling modifications, material changes, or processing adjustments.
What Makes a Reliable Tooling Supplier?
Selecting a supplier should involve more than comparing quotations.
A reliable Injection Mold Tooling China company should demonstrate strong engineering, manufacturing, and quality-control capabilities.
Important factors to evaluate include:
- Previous mold-making experience
- Available CNC and EDM equipment
- Engineering support
- Mold material traceability
- Inspection capabilities
- Mold-testing process
- Communication quality
- Production capacity
- Documentation
- Tool maintenance support
Requesting examples of similar previous projects can also help businesses understand whether the manufacturer has relevant experience.
Quality Control for Plastic Injection Parts
Consistent quality requires inspection throughout production.
Depending on the product, manufacturers may check:
- Length and width
- Hole dimensions
- Critical tolerances
- Component weight
- Surface finish
- Color
- Assembly performance
- Functional dimensions
Advanced components may require coordinate measuring machines or optical measurement systems.
Inspection data can help identify production variation before large quantities of defective components are manufactured.
For high-volume Plastic Injection Parts, process stability is just as important as inspecting individual samples.
How Businesses Can Prepare for a Tooling Project
Providing complete information helps tooling manufacturers prepare better solutions.
Before requesting a quotation, businesses should ideally prepare:
- 3D CAD model
- 2D engineering drawing
- Plastic material specification
- Required color
- Surface finish
- Critical tolerances
- Expected production quantity
- Annual demand
- Assembly requirements
- Special testing requirements
Clear information reduces assumptions and allows the supplier to design tooling that matches actual production expectations.
Frequently Asked Questions
1. What is Injection Mold Tooling China?
Injection Mold Tooling China refers to injection mold design and manufacturing services provided by tooling manufacturers based in China.
2. What are Plastic Injection Parts?
Plastic Injection Parts are components formed by injecting molten plastic into specially engineered mold cavities.
3. How long does an injection mold last?
Mold life depends on mold steel, resin type, component complexity, maintenance, production conditions, and tooling quality.
4. Can injection molding produce complex products?
Yes. Slides, lifters, inserts, and other mold mechanisms can be used for complicated component geometries.
5. Which materials can be injection molded?
Common materials include ABS, PP, PC, nylon, POM, PE, TPE, and various engineering polymers.
6. Why is draft angle required?
Draft helps molded components release smoothly from the mold without unnecessary scratching or damage.
7. What is a mold trial?
A mold trial is a test production run used to evaluate mold performance and inspect sample parts before mass production.
8. Are multi-cavity molds better?
They can improve productivity for large production volumes, but the best choice depends on product size, complexity, demand, and budget.
9. Can molded plastic parts have textures?
Yes. Mold surfaces can be polished, textured, engraved, or treated to create different appearances.
10. How can injection molding costs be controlled?
Optimizing component design, cavity quantity, material choice, tooling structure, and cycle time can help control overall manufacturing costs.